Continuous consolidation
Multi-ply prepreg is continuously fed, heated, compacted and cooled to manufacture flat laminate. CARO has actual production experience with laminate for buoys.
 한국어
From multi-ply prepreg to structural laminate. Connecting heating, consolidation and cooling in a continuous process.
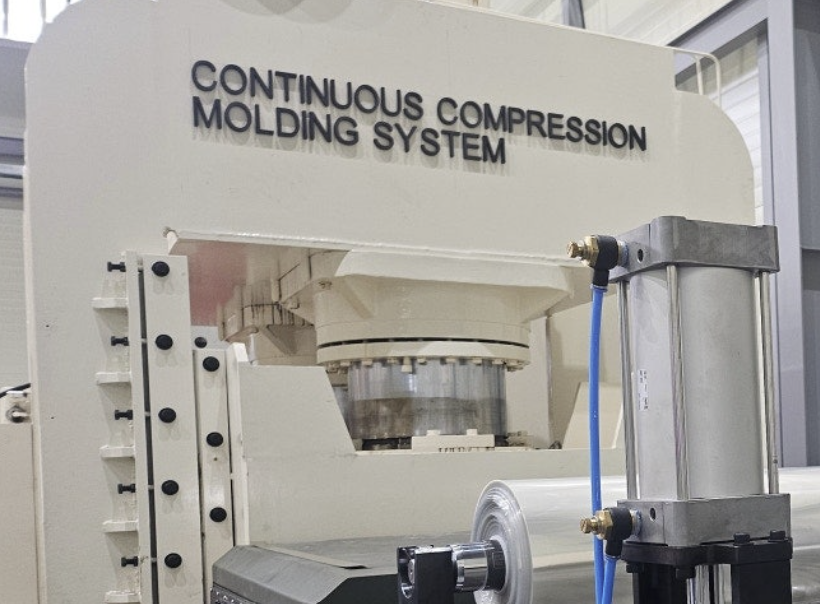
Multi-ply prepreg is continuously fed, heated, compacted and cooled to manufacture flat laminate. CARO has actual production experience with laminate for buoys.
CONTINUOUS PROCESS
From multi-ply prepreg rolls to consolidated structural laminate, material feeding, heating, compression, cooling and cutting form a continuous workflow.
Eight prepreg rolls feed the multi-ply material continuously. The design allows further expansion; actual ply count and thickness are reviewed against the feed configuration.
IR preheating prepares the layup for heated consolidation. Conditions are set according to material, thickness and feed requirements.
Already polymerized thermoplastic prepreg is heated and compressed to consolidate the multi-ply structure. This stage uses thermoplastic consolidation rather than waiting for resin cure.
The consolidated material is cooled to produce laminate. Cooling conditions are reviewed against thickness and feed requirements.
Continuous feeding connects heating, consolidation, cooling and cutting. Feed conditions are reviewed together with heating and cooling requirements.
Laminate is automatically cut to the customer-specified length. Separate narrower-width cutting can be considered for the supply specification.
The diagram shows the functional flow based on the equipment configuration. Continuous feeding connects the process stages. Temperature, pressure, speed and residence time are managed for each product; public values: [ ].
1,000 mm width, an eight-roll unwinder with provision for expansion, IR preheating, continuous compression, heating/cooling, feeding and automatic cutting.
Cut-to-length supply is supported. Thickness and layup conditions are reviewed together with the material and equipment constraints.
CCM LAMINATE SPECIFICATIONS
| Item | Specification / confirmation status |
|---|---|
| Manufacturing width | 1,000 mm |
| Normal thickness range | 0.2–3.0 mm · subject to specification and process review |
| Maximum thickness produced to date | 2.0 mm · distinct from an absolute equipment limit |
| Ply feeding | Eight-roll unwinder · provision for expansion |
| Supply length | Customer-specified set length → automatic cutting |
| Narrow-width supply | Narrower-width cutting available when required |
| Continuous feed / production speed | Reference speed: 1 m/min · actual operating speed is adjusted for material, thickness, heating and cooling conditions |
| Dimensional tolerances | Thickness, width and length: [ ] |
| Custom thick sheets | 15 mm, 20 mm and other thick sheets: separate heated press consolidation, outside the continuous CCM specification |
Basis: user-confirmed specifications and the CCM construction report. Page 16 records 1.8–2.0 mm thickness in a six-ply commissioning trial. This trial result is not a general tolerance for all products.