Integrated Manufacturing Automation connects material preparation, forming and downstream operations into one integrated manufacturing workflow.
CARO automation that connects the process
Integrated Manufacturing Automation connects material preparation, drying, preheating and transfer, compression forming, trimming/piercing, joining and stacking. It integrates material transfer and operations across stages, extending beyond individual forming equipment.
INTEGRATED MANUFACTURING PROCESS
Integrated manufacturing process flow
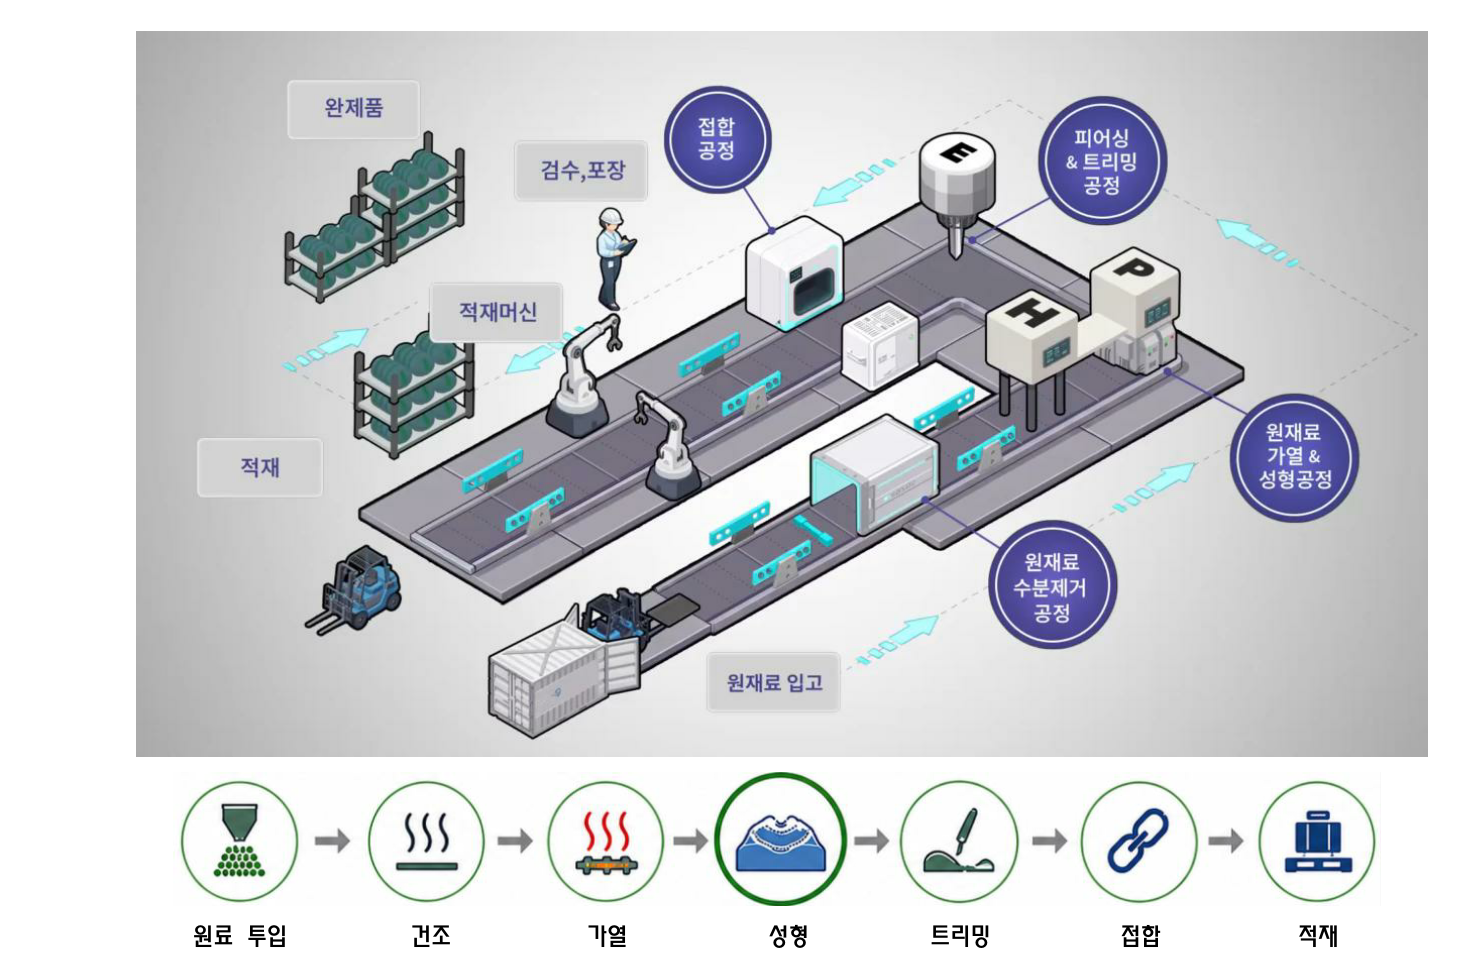
Configuration diagram of the implemented buoy manufacturing automation process. Select the image for a larger view. Original Korean labels are retained.
01Material preparation & feeding
02Drying & moisture management
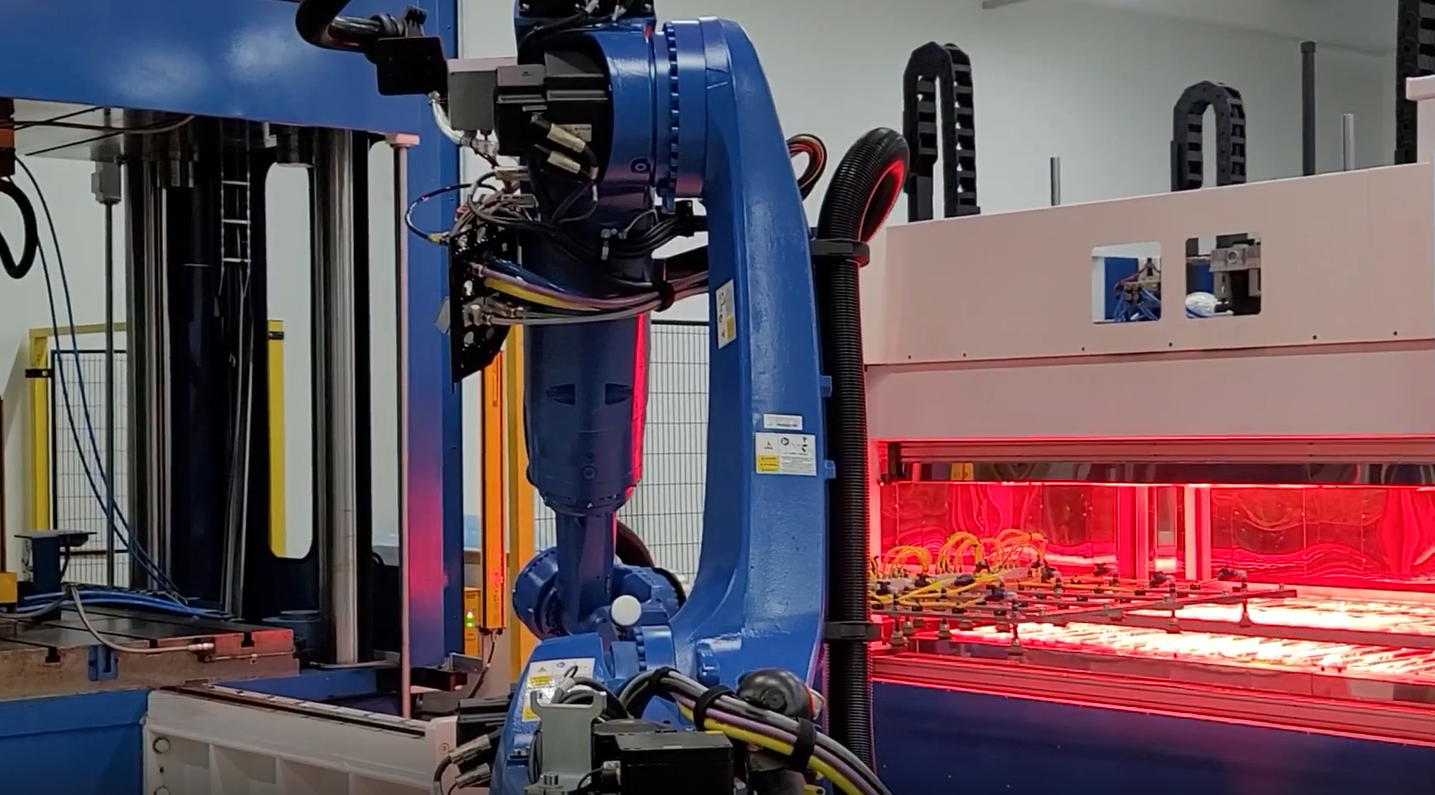
03Preheating & transfer
04Compression forming & cooling
05Trimming & piercing
06Joining
07Stacking, inspection & packing
The diagram describes the functional sequence. Its heating/forming section is explained as preheating/transfer and compression forming/cooling. Trimming and piercing are downstream product operations, distinct from standard laminate supply.
Features of each process stage
01
Material preparation & feeding
Prepreg or laminate is prepared and fed according to the product specification. Material configuration and placement are coordinated with preheating and forming conditions.
02
Drying & moisture management
The drying stage manages the material moisture condition. Drying requirements are reviewed for the material and its storage condition.
03
Preheating & transfer
Material is heated to a state suitable for forming and transferred to the press mold. The preheated state, heat loss during transfer and loading position are considered together.
04
Compression forming & cooling
Pressure forms the part in the mold, followed by cooling. Material and mold temperatures, pressure, cooling and demolding conditions are reviewed as one forming cycle.
05
Trimming & piercing
Edges and geometry are finished after forming, with piercing where required by the product design. Machining positions and geometry needed for joining are reviewed together.
06
Joining
Formed components are joined to suit the product structure. Joint location, alignment, method and conditions are reviewed for each product.
07
Stacking, inspection & packing
Finished parts are stacked and connected to inspection and packing. Automation scope and operator checking/handling roles are reviewed against the workflow configuration.
The focus of integrated automation
Process integration
Connect preheated material transfer and downstream operations into a repeatable workflow.
Coordinated thermal and forming conditions
Review preheating, mold temperature, pressure, cooling and transfer conditions together.
Product-specific process design
Review tooling and automation scope against product geometry, materials, joining and finishing requirements.
Implementation status and refinement
The full buoy manufacturing workflow has been implemented, with actual buoy fabrication and aquaculture-site installation experience. Process conditions and equipment are being refined. Full workflow implementation is distinguished from fully unmanned operation.
Public values for stage-specific automation scope, cycle time, output and inspection criteria: [ ].