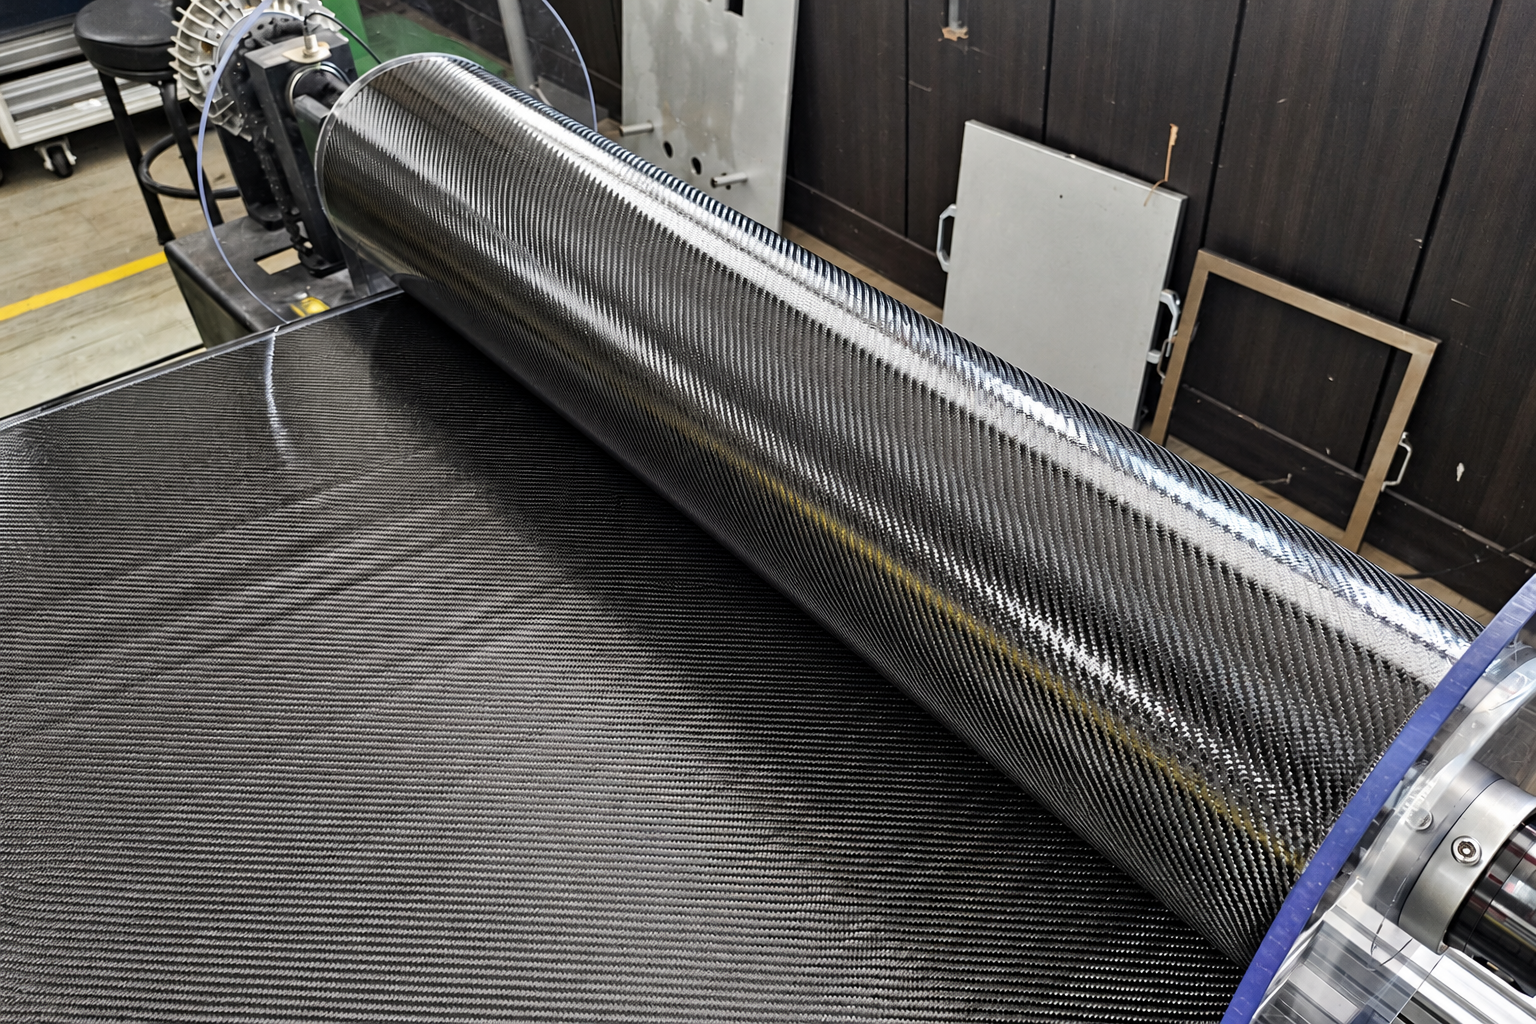
A flexible single-ply woven intermediate combining Carbon, Basalt or Glass fabrics with Elium® acrylic thermoplastic resin. The fully polymerized, tack-free prepreg is supplied in rolls for subsequent layup and heated consolidation.
KEY FEATURES & BENEFITS
Key Features & Benefits
Flexible single-ply roll supply
Flexible woven prepreg is supplied in rolls for layup and continuous feeding.
Tack-free handling
Fully polymerized, tack-free supply supports convenient handling and layup.
Lightweight structures and strength
Fiber reinforcement and layup design support lightweight structures with the strength and stiffness required for the application.
Reprocessing and reforming
Thermoplastic resin enables subsequent forming and reforming to be considered under appropriate heating conditions.
Impact and damage performance
Fiber, resin and layup choices can address impact and damage requirements. Performance is verified for the specific application.
Chemical resistance and service temperature
Resin and structural choices are reviewed for suitability under chemical exposure and service-temperature conditions.
Recycling and repair possibilities
Thermoplastic materials support consideration of recycling, reprocessing and repair routes, selected according to the product structure and conditions.
Manufacturing and forming efficiency
Already polymerized prepreg is heated and consolidated into products, with routes to continuous consolidation and press forming.
Customization for the application
Carbon, Basalt and Glass materials, plain and twill fabrics, thickness and layup are reviewed for the intended product.
Cost efficiency
Material use, layup, manufacturing processes and automation are considered together to improve development and production cost efficiency.
Actual performance and benefits depend on materials, layup, processing and the service environment. Numerical and comparative performance will be added when product-specific test data are available.
THERMOPLASTIC ADVANTAGES
How CARO differs from thermoset materials
Less expiry management · Shorter subsequent forming · Continuous production and automation
Comparison
CARO thermoplastic prepreg / laminate
Typical thermoset prepreg / laminate
Storage and expiry
Fully polymerized solid prepreg requires no refrigerated or frozen storage and has no expiry caused by the progress of uncured-resin curing.
Uncured prepreg requires resin-specific shelf/out-life management and may require cold storage. The same uncured-resin expiry concept does not apply to fully cured laminate.
Subsequent forming principle
Already polymerized material is heated, consolidated/formed and cooled, without waiting for a separate resin cure at this stage.
Prepreg layup requires chemical resin curing; post-curing may be included depending on the system.
Processing time
Eliminating the cure wait in subsequent forming supports shorter cycle design. Actual time depends on thickness, heating and cooling.
Cure time and sometimes post-cure time are required. Rapid-curing thermoset systems also exist; comparisons must be process-specific.
Continuous production and scalability
Roll-prepreg feeding, continuous CCM laminate manufacture, automatic cutting and press automation support repeatable production.
Cure conditions and material out-life must be incorporated into planning. Thermosets can also support automated, continuous and high-volume processes.
Inventory and handling
Avoids cold-storage and thawing requirements; tack-free handling supports storage, feeding and layup.
Prepreg may require cold-chain logistics, thawing and out-time tracking. Cured laminate follows separate handling requirements.
Thick laminates
No cure exotherm must be controlled during heated consolidation. Thick sheets are reviewed in a separate press for heat transfer, pressure and cooling.
Cure exotherm and heat transfer inform the cure schedule. Thick sheets are possible, with appropriate process control.
Changes after forming
Reheating and reforming can be considered under material- and structure-appropriate conditions.
Cured resin is difficult to reform through reheating in the manner of a thermoplastic.
Recycling
Thermoplastic behavior supports consideration of reprocessing and recycling routes.
The cured crosslinked matrix does not readily remelt; separate recycling routes are required.
The expiry statement applies to already polymerized CARO products, not to the storage life of liquid Elium® resin before manufacture. Moisture, contamination, UV and heat exposure remain storage considerations. Guaranteed storage period and quantified cycle time/output: [ ]. Comparisons describe general principles and depend on the resin and process.
Developed using CARO’s patent-related manufacturing technology, Carbon/Elium®, Basalt/Elium® and Glass/Elium® are representative prepreg product families. Material selection draws on a range of fabric specifications to suit the customer’s application, performance requirements and forming process.
IMPREGNATE FIRST · POLYMERIZE IN PLACE
How in-situ polymerization impregnation benefits prepreg
Impregnate in a low-viscosity liquid state, then form the thermoplastic polymer within the fabric.
01Fabric feeding
02Low-viscosity liquid impregnation
03In-situ polymerization
04Winding polymerized prepreg
05Cutting & layup
06Heated consolidation & cooling
01
Low-viscosity impregnation into the fibers
Liquid acrylic thermoplastic resin impregnates the fabric first, reducing the impregnation challenge associated with highly viscous polymer melts. This approach supports control of wetting within fiber bundles and resin distribution.
02
Polymerization within the fabric
The impregnated resin is polymerized within the fabric to form a solid thermoplastic matrix. Connecting low-viscosity impregnation with polymer formation is the core of the process.
03
A flexible, tack-free intermediate
Fully polymerized fabric prepreg is handled as a flexible single-ply intermediate and supplied in rolls. Customers can cut and lay it up for subsequent heated consolidation.
04
Reduced cold-storage requirements
As an already polymerized solid prepreg, it avoids uncured thermoset cure-related expiry management and cold-storage requirements. Storage-environment controls and a formal guaranteed period remain separate considerations.
05
From continuous manufacture to continuous forming
Fabric feeding, impregnation, polymerization and winding connect in a continuous manufacturing workflow. Supplied rolls can then feed multi-ply CCM, linking material manufacture with laminate consolidation.
06
Shorter downstream forming workflow
Polymerization is completed before prepreg supply, allowing subsequent forming to use heating, consolidation and cooling. Polymerization during material manufacture and later thermoforming are distinct stages.
This explanation summarizes the manufacturing principle and customer benefits from the supplied technical notes and CARO product definition. Specific patent protection must be checked against the final claims. Quantitative comparisons of impregnation uniformity, void content, properties and productivity: [ ]. Specific resin grades, formulations and polymerization conditions are confidential.
PATENT-RELATED TECHNOLOGY
Patent-related prepreg manufacturing technology
고분자 복합재 제조 장치 및 제조 방법
Apparatus and method for manufacturing polymer composites (descriptive English translation). A decision to grant has been issued for this invention related to CARO manufacturing technology.
Applicant
주식회사 복합재자동화기술
Application number
10-2025-0110342
Verified status
Decision to grant issued · based on the supplied decision document
Registration number
[ ] · pending registration confirmation
The title and application number follow the supplied decision document. Registration number, registration date and product-related claim scope will be added after confirmation.
Data and specifications
Specific resin grades, formulations and manufacturing conditions are confidential. Supply specifications and technical data are reviewed against the intended use. Pending specifications: [ ].